Hey there, if you’re reading this, chances are you’ve either worked with aluminum die casting parts before, or you’re in the market for a reliable supplier to get them made right. As someone who’s spent the last decade running our small, shop-floor-focused aluminum die casting parts business (yep, I’m the guy who still pulls 12-hour shifts on the floor when we’re cranking out orders), I’ve seen first-hand how a little early design thought can save you hundreds, maybe thousands of dollars, tons of headaches, and way too many late nights fixing mistakes. Let’s cut the corporate jargon—today we’re talking about the real, practical design considerations for aluminum die casting parts, the stuff we check twice before hitting that “send to production” button on a new order. Aluminum Die Casting Partsr
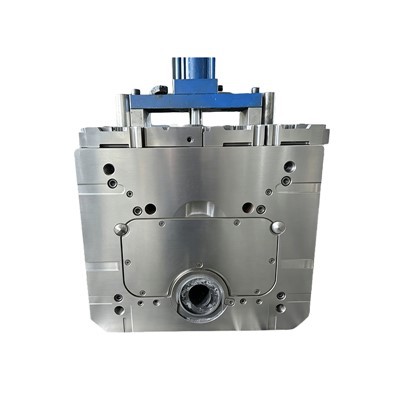
First off, let’s get one thing straight: aluminum die casting isn’t the same as 3D printing or machining raw aluminum. When we force molten aluminum (heated to like 1,200°F, hot enough to melt steel tools over time) into a steel mold at 10,000+ PSI, the part’s design has to play nice with that process from start to finish. If you skip these steps, you’re gonna end up with parts that have tiny air bubbles that make them weak, or edges that break off when you eject them from the mold, or even parts that cost way more than they need to because we have to machine away 20% of the material just to fix defects. Let’s start with the big one: wall thickness. This is probably the single most important thing we yell about when we’re talking to clients about new designs.
Here’s the thing: aluminum doesn’t cool evenly. If one section of your part is super thick, and another is paper-thin, the thick parts will take forever to cool, which means molten aluminum gets stuck in the thin spots and doesn’t fill the mold right. That’s called cold shuts, and they’re a pain to fix—sometimes we have to scrap a whole mold insert just to adjust that section. The sweet spot for most aluminum die casting parts is between 2mm and 5mm. Wait, hold on—before you think, “My part has a 10mm thick boss, what do I do?” That’s totally fine, but don’t make that boss solid. We always machine a small hole in the center of thick features like bosses or mounting pads. It reduces the mass so it cools at the same rate as the rest of the part, and it also cuts down on material use, which makes the part cheaper for you. We had a client last year who sent us a design for a bracket with a solid 12mm thick mounting point. He thought it was sturdier, right? But when we quoted it, the price was 30% higher than what he expected. We explained why, redesigned that boss to have a 4mm core hole, and he saved almost $2,000 on a 1,000-part order. That’s the kind of win we live for.
Next up: draft angles. I know, I know—draft angles sound like something from a high school geometry class you skipped, but trust me, they make or break the part. When the molten aluminum cools, it shrinks just a little (like 0.5% to 0.7% for aluminum, depending on the alloy), and that shrinkage makes the part stick to the inner walls of the steel mold. If there’s no draft angle, when we eject the part with a hydraulic pin, it’s gonna snap. We don’t want that, and you don’t want a whole batch of broken parts. The rule of thumb? For vertical walls that you look at as flat surfaces on the part, 0.5 degrees per side for small parts, and up to 1 degree per side for larger parts. Even 0.25 degrees works for tiny, simple features, but don’t go below that. We had a client once who sent a design with 0.1 degrees draft on a 6-inch long part, and we had to throw out the whole first mold trial—every part got stuck and broke when ejecting. We had to remachine the mold inserts to add the right draft, which delayed his order by 5 days and cost him extra. It’s such an easy fix, but people sleep on it all the time.
Then there’s undercuts. Let’s be real, undercuts are the parts of your design that stick out or go inward in places that the standard mold can’t get to. If you have a hole that’s deeper than its diameter, or a tab that sticks out perpendicular to the part’s main surface, you’ve got an undercut. The problem with undercuts? They require us to add extra parts to the mold, like slides or lifters, which adds time and cost to the tooling. And if you have too many undercuts, or really complex ones, the mold becomes way more prone to breaking over time. We once had a client with a part that had 8 tiny internal undercuts, and the mold for that part costs twice as much as a standard mold for a similar size part. The client thought it was worth it, but by the end of the production run, the slides were wearing out so bad we had to replace them every 10,000 parts, which drove up the per-part cost. The fix here is simple: if you can adjust the undercut to something that can be molded without extra inserts, do it. Even a tiny change, like making an undercut into a slight draft with a small feature at the end, can save you a ton. If you can’t get rid of the undercut, be upfront about it with your supplier early on—don’t wait until the tool design is almost done to say, “Oh, I need this weird bump here.” It only makes the process slower.
Another big one is radii and corners. Sharp corners sound harmless, right? I mean, they’re just corners. But here’s the thing: in the mold, sharp corners create stress concentrations. When you inject molten aluminum, the flow gets choked off at sharp corners, leaving tiny voids inside that make the part weaker. And when the part is cooling, those sharp corners are where cracks start to form during ejection or later, when the part is in use. We always tell clients to replace all sharp 90-degree corners with a radius of at least 1mm, even for small parts. For edges that are under tension or load—like mounting points or areas where parts connect to each other—make that radius even bigger, like 2mm or 3mm. We had a client who wanted a bracket for a trailer hitch with sharp corners, thinking it would fit better into his assembly. We did the first run with sharp corners, and 15% of the parts cracked when he bolted them on. We had to re-machine the mold to add radii, re-run the whole batch, and he paid us nothing extra because we should’ve caught that in the design review. That’s a mistake we don’t make again—now we flag every sharp corner in a design before we even open the mold software.
Wait, let’s not forget about part geometry and alignment. When you’re designing parts that fit together with other components—like housings that hold electronics, or brackets that bolt to other metal parts—you have to account for how die casting tolerances work. Aluminum die casting is accurate, but not perfect. The standard tolerance for a die cast part is around ±0.1mm for small parts, and up to ±0.2mm for larger parts. If you need something tighter, like a hole that has to line up with another part exactly, you’ll have to specify that, and it will cost more because we have to inspect each part more carefully, or add secondary machining to get the tolerance right. We recently had a client who sent a design for a pump housing with holes that needed to line up with a motor shaft within 0.05mm. Without us catching it early, we would’ve run the whole batch, and half of them would’ve not fit. We told him upfront that the extra tolerance would add 15% to the part cost, and he was grateful we caught it instead of getting stuck with a bunch of unusable parts. Also, avoid long, thin features that stick out a lot—they can warp during cooling, especially if the wall thickness is uneven. If you have a long tab or a thin fin, add a small rib to reinforce it without adding too much material, that will keep it straight and strong.
Oh, and alloy selection! This is a big one that a lot of clients skip over. Not all aluminum alloys are the same for die casting. Some are great for strength, some are great for corrosion resistance, some are cheap and easy to cast. If you’re making a part that goes outside, like a fence bracket or a car component, you’ll want a corrosion-resistant alloy like A380, which is the most common one we use—good castability, decent strength, and holds up to weather. If you need something stronger for structural parts, like a truck frame component, go for A356, which has higher tensile strength, but it’s a little more expensive and a bit harder to cast. And if you’re making parts that hold electronics, like a laptop housing, you might want an alloy that has good thermal conductivity, like ADC12, which is also good for detail work. The worst thing someone can do is pick a random alloy without thinking about the part’s use case. We had a client last year who used a cheap, low-grade alloy for a part that went on a marine water pump—within 3 months, the part corroded through. He blamed us, but it turned out he picked an alloy that wasn’t rated for saltwater exposure. We worked with him to switch to A380, which is corrosion-resistant, and fixed his problem, but that’s the kind of mistake that could’ve been avoided with a little planning.
Wait, let’s talk about gating and overflow locations, too. I know that’s mold design stuff, but it affects your part’s design. Gating is where the molten aluminum flows into the mold, and overflow locations are where we trap any air or impurities that would otherwise get stuck in your part. If your part has a thin section or a complex feature, we’ll place the gate in the thickest area of the part, so the molten aluminum flows through the thick section first and fills the rest of the mold evenly. If you have a small hole or a fine detail, don’t put the overflow right next to it—you’ll ruin the detail. Most of the time, we have to adjust the gate location based on the part’s geometry, so the earlier we get your design, the more we can work with you to place gates and overflows in spots that don’t interfere with your assembly.
And let’s not skip secondary operations—things like machining, plating, or painting. If your part needs to have a flat surface that’s perfectly smooth, or a hole that needs to be tapped, you have to account for that in your design. Don’t design a hole that’s too close to the edge of the part if you’re gonna machine it—you’ll end up with a weak edge that chips. If you’re plating or powder coating the part, make sure the walls aren’t too thin, because thin walls can warp when they’re heated during coating. We always add a note to every design review: “These sections will work great for machining” or “This area is tricky to plate, can we adjust it?” so you don’t have to deal with rework later.
Let’s be real— I get it, you’re not a die casting expert. You’re a product designer, a procurement manager, an engineer, you just need parts that work, that are made on time, that don’t break the bank. The number one mistake we see is waiting until the design is 100% done before talking to a die caster. By the time you send us the final design, it’s way harder and more expensive to fix small issues. If you talk to us early, we can tweak the design to be more castable, save you money, avoid delays, and make a better part.
At the end of the day, aluminum die casting is all about balance. Balance between wall thickness, draft angles, undercuts, geometry, and alloy selection. It’s not rocket science, but it requires paying attention to the details that make the process work. We’ve been doing this for years, we’ve fixed more bad designs than I can count, and we know how to make your parts work right, the first time.
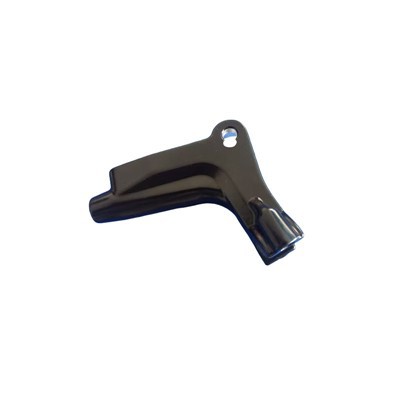
If you’re working on a new project, or you have a design that’s not performing the way you want, reach out. We don’t do pushy sales calls, we just look at your design, tell you what works, what doesn’t, and give you a real quote without the hidden fees. We want to make this easy for you, because when your parts work, you’ll come back, and that’s the only way we do business.
Die Casting Parts References:
- Die Casting Design Guidelines, American Die Casting Association
- Aluminum Alloys for Die Casting: Properties and Applications, Aluminum Association
- Tolerance Standards for Die Castings, International Organization for Standardization (ISO 8062-3)
Suzhou Ruide Die-Casting Mold Co., Ltd.
Address: No.2, Wanchen Road, Huayang Village, Wangting Town, Xiangcheng District, Suzhou City, Jiangsu Province
E-mail: jada@cnrdmj.com.cn
WebSite: https://www.cnrdmold.com/
